Factory Images
Company Introduction
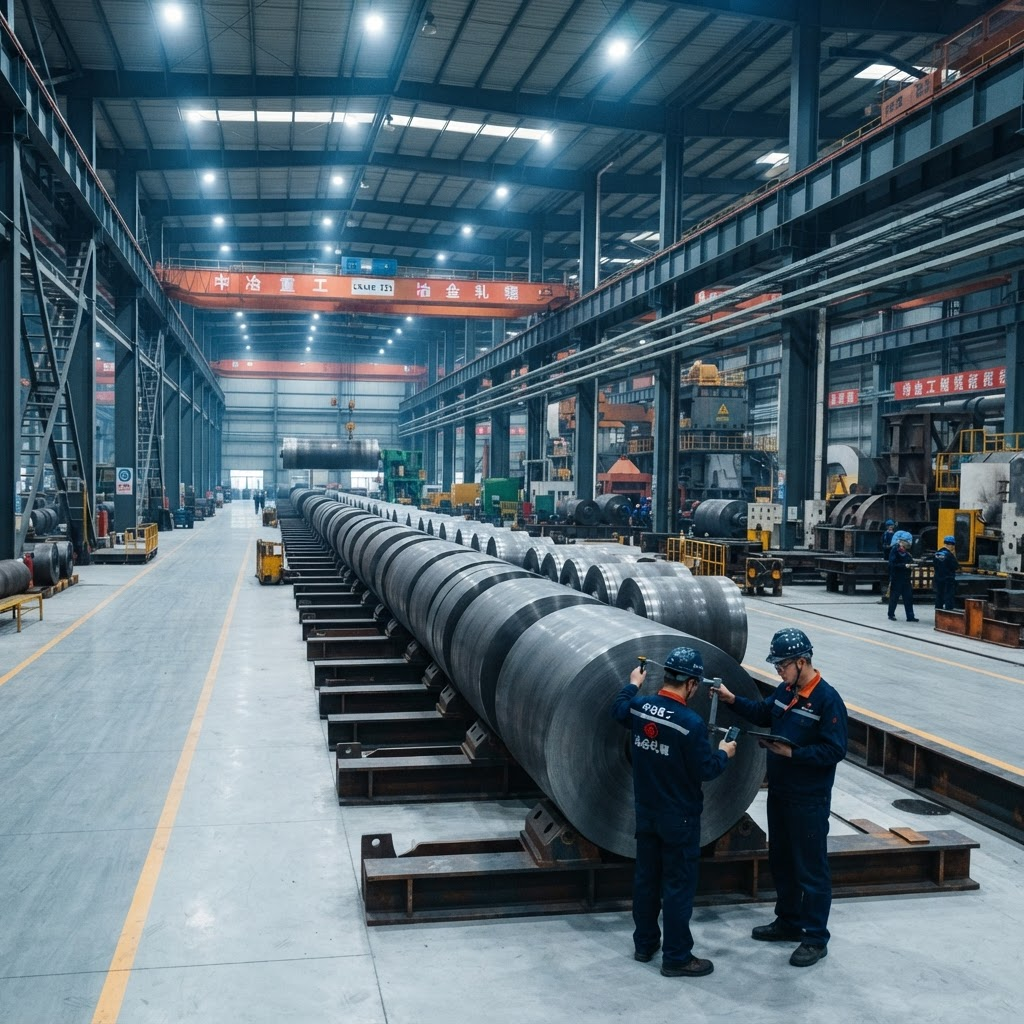
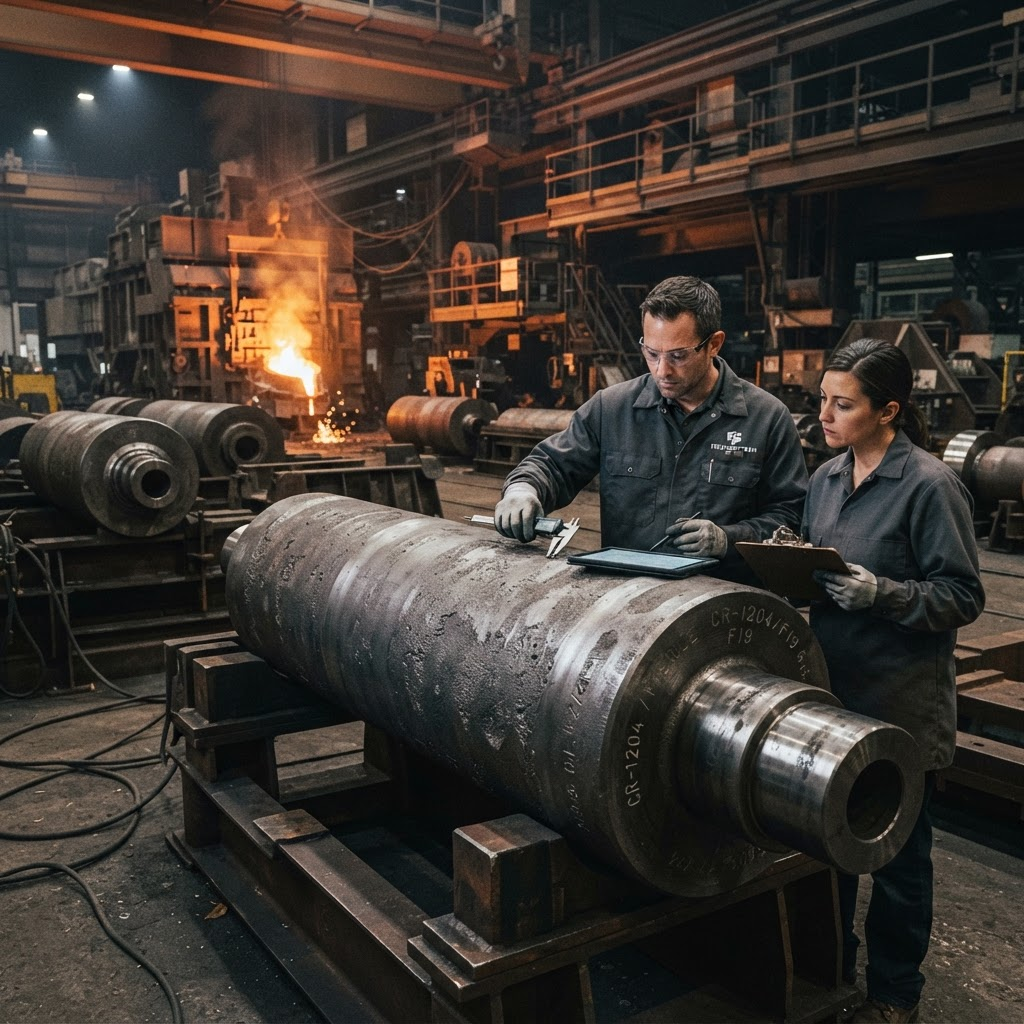
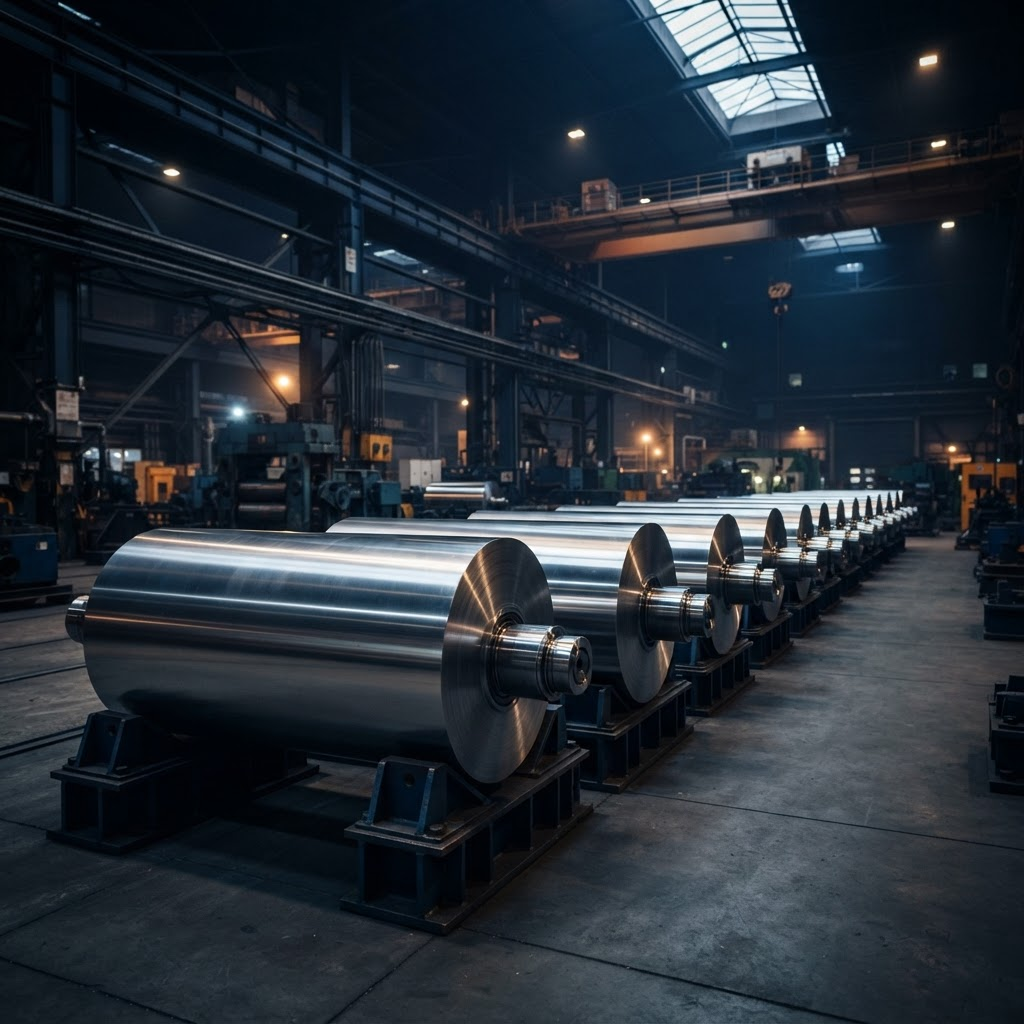
Founded in 1998 in Changzhou, Jiangsu Province, Changji has built over two decades of expertise in cast roll metallurgy. The facility operates dedicated centrifugal casting lines and static casting facilities, supported by a fully equipped metallurgical laboratory for alloy development and quality verification. Rolls produced by Changji serve roughing, intermediate, and finishing stands across hot strip mills, plate mills, section mills, bar mills, and wire rod lines. VSAG partners with Changji to bring this proven casting technology to Indian steel producers.
Technology
Centrifugal Casting
Horizontal and vertical centrifugal casting lines produce composite roll shells with hard outer shell and tough core — the foundation of ICDP and Hi-Cr roll performance.
Static Casting
Gravity static casting for large-diameter and complex geometry rolls where centrifugal casting is not applicable.
Controlled Cooling & Annealing
Precise temperature-controlled cooling tunnels and annealing furnaces develop the carbide microstructure and relieve residual stresses in finished rolls.
CNC Roll Grinding
In-house CNC cylindrical grinding to final dimensional tolerance and surface finish, with groove milling for long-product roll profiles.
Products Manufactured
- Indefinite Chilled Double Pour (ICDP) Rolls
- High Chromium Iron (Hi-Cr) Rolls
- Spheroidal Graphite (SG) Iron Rolls
- Nickel Hard (NI-Hard) Rolls
- Semi-High Speed Steel (Semi-HSS) Rolls
- Grooved Bar & Section Mill Rolls
Manufacturing Process
- 01
Alloy Design
Customer specification reviewed and alloy composition set in metallurgical lab, including carbon, chromium, nickel, and molybdenum adjustments for target hardness.
- 02
Melt Preparation
Electric induction furnace melting with precise alloy additions, temperature control, and degassing to achieve target chemistry.
- 03
Casting
Centrifugal or static casting into prepared moulds, with controlled pour temperature and rotation speed for composite shell rolls.
- 04
Controlled Cooling
Rolls are cooled in tunnel furnaces under programmed cooling curves to develop the target microstructure and minimise residual stress.
- 05
Rough Machining
Turning and boring to remove casting skin, establish datum surfaces, and prepare the roll for heat treatment inspection.
- 06
Annealing & Stress Relief
Final heat treatment cycle to stabilise microstructure, relieve machining stresses, and achieve final hardness target.
- 07
Finish Grinding
CNC cylindrical grinding to final dimension, cylindricity, and surface finish. Groove milling for long-product rolls to customer groove drawing.
- 08
Inspection & Certification
Full hardness survey, ultrasonic testing, surface inspection, and dimensional report issued. Certificate of conformance and material certificate provided.
Quality Control
Hardness Mapping
Shore D hardness measured at multiple points across the barrel surface to confirm uniformity within specification.
Ultrasonic Testing (UT)
Volumetric UT inspection of roll shell and core to detect internal defects including porosity, inclusions, and cracks.
Microstructure Analysis
Metallographic examination of representative sections to confirm carbide distribution and graphite morphology against specification.
Chemical Analysis
Optical emission spectrometry (OES) analysis of each heat to verify alloy chemistry against the order specification.
Dimensional Inspection
CMM and precision gauging of all critical dimensions — diameter, cylindricity, straightness, neck dimensions — against customer drawing.
Certifications
- ISO 9001:2015 — Quality Management System
- ISO 14001 — Environmental Management
- SGS Third-Party Inspection Approved
- BV (Bureau Veritas) Approved Manufacturer
Location
Changzhou, Jiangsu Province, China
Xinbei District, Changzhou, Jiangsu Province, 213000, P.R. China
Downloads
Available upon enquiry. Contact VSAG to request partner documentation.
Products Supplied Through VSAG
Work Rolls
High-performance work rolls engineered for hot and cold rolling mills, delivering consistent surface quality and extended campaign life.
View product
Cast Rolls
Durable cast rolls in a range of metallurgical grades, produced by certified foundry partners for reliable performance.
View product